Search News
Industry Portal
Hot Articles
- When does wholesale spark plug pricing justify buying in bulk?Spark plugs wholesale can cut costs when demand, fitment, traceability, and storage align. Learn the break-even factors for smarter bulk buying.
- How to evaluate an electromagnetic protection materials distributorEvaluate an electromagnetic protection materials distributor with confidence. Compare technical evidence, traceability, supply resilience, compliance support, and total lifecycle value.
- How conductive gaskets improve EMI protection for cable assembliesEMI protection for cable assemblies starts at the interface. Learn how conductive gaskets improve shielding continuity, bonding, compression control, and long-term EMC reliability.
UV curable glue vs thermal bonding for assembly
Time
Click Count
Choosing the optimal assembly method is critical for ensuring long-term Structural Durability in high-stakes infrastructure. This technical comparison between UV curable glue and thermal bonding evaluates how each process impacts Structural Safety and the performance of advanced Engineering Materials. At G-SCE, we analyze how these Material Fabrication techniques integrate with EMI Mitigation strategies and Shielding Protocols to protect critical assets. For project managers and technical evaluators, selecting between adhesives and thermal methods affects everything from Infrastructure Materials integrity to the effectiveness of Industrial Fasteners and Seismic Protection systems. Understanding these nuances is essential for implementing robust Structural Repair solutions and maintaining the rigorous standards required for modern, large-scale engineering projects.
Understanding the Fundamental Mechanisms: UV Curing vs. Thermal Fusion
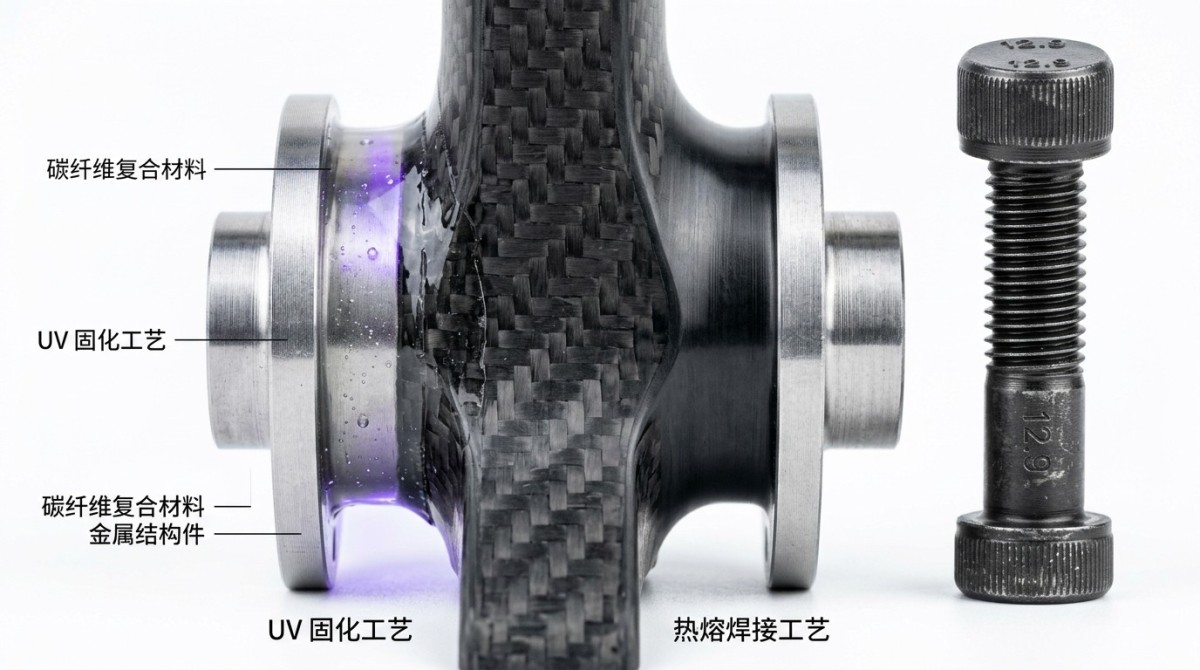
UV curable adhesives represent a pinnacle of modern chemical engineering, relying on a process known as photopolymerization. When exposed to specific light wavelengths, typically within the 365nm to 405nm range, photoinitiators within the adhesive trigger a rapid chain reaction. This converts the liquid resin into a solid cross-linked polymer matrix in a matter of seconds. For structural engineers and technical evaluators, the primary appeal lies in this near-instantaneous transition, which allows for immediate handling and further assembly steps. This mechanism is particularly advantageous in precision electronics and aerospace components where high-speed throughput is essential without compromising the structural integrity of sensitive shielding gaskets or delicate fiber-optic connectors.
In contrast, thermal bonding—often referred to as heat sealing or fusion bonding—relies on the application of controlled thermal energy to melt or soften the interface between two substrates. This process usually occurs at temperatures ranging from 150°C to over 350°C, depending on whether one is working with thermoplastic polymers or high-performance thermosetting resins. As the materials reach their glass transition temperature or melting point, molecular diffusion occurs across the interface, creating a cohesive bond that, once cooled, often equals the strength of the parent material. For decision-makers managing mega-structures, thermal bonding provides a level of molecular homogeneity that is difficult to replicate with chemical adhesives, especially in high-stress seismic isolation units.
The choice between these two methods is often dictated by the thermal sensitivity of the surrounding infrastructure components. While thermal bonding creates exceptionally robust joints, the required heat can induce thermal stress or deformation in nearby high-precision industrial fasteners or electromagnetic shielding materials. UV curing, being a "cold" process, eliminates the risk of heat-affected zones (HAZ), making it the preferred choice for assembling hybrid materials where disparate coefficients of thermal expansion (CTE) could lead to catastrophic failure under cyclic loading. Understanding these basic physics is the first step for procurement directors in balancing production efficiency with century-long lifecycle durability.
Furthermore, the environmental conditions of the fabrication site play a significant role. UV curing requires a direct line of sight to the light source, which can be a limitation for complex, shadowed geometries found in internal structural reinforcement. Thermal bonding, while requiring more energy and specialized containment, can often be applied through conduction or induction in areas where light cannot reach. Project managers must evaluate the accessibility of the bonding site alongside the required cure speed to determine which methodology aligns with the project's safety and shielding protocols, especially when dealing with Grade 12.9 specialized bolts and complex seismic bearings.
Comparative Performance Metrics for Structural Integrity
When benchmarking these assembly techniques against international standards such as ISO 9001 and ASTM D1002, the performance metrics reveal distinct trade-offs. UV curable glues excel in precision and process control, offering a typical tensile strength range of 20 MPa to 40 MPa. However, their performance can degrade if the UV intensity is not strictly monitored, leading to incomplete polymerization. For quality control managers, this necessitates the implementation of rigorous 100% inspection protocols using radiometers to ensure every bond receives the mandatory dosage, typically measured in Joules per square centimeter (J/cm²).
Thermal bonding, on the other hand, is often measured by its ability to maintain integrity under extreme environmental saturation. In many aerospace applications, thermal fusion joints must withstand continuous operating temperatures of 200°C while maintaining 90% of their original shear strength. This makes thermal methods indispensable for components located near engine exhausts or within high-voltage electromagnetic interference (EMI) environments where organic adhesives might outgas or degrade over a 50-year service life. Procurement directors must weigh these long-term reliability factors against the higher initial capital expenditure (CAPEX) required for industrial furnaces or induction heaters.
The following table provides a high-level technical comparison designed to assist technical evaluators and chief infrastructure officers in their decision-making process for large-scale engineering assets.
As evidenced by the comparison above, UV curable systems offer a significant advantage in throughput, reducing assembly cycle times by over 90% in many scenarios. However, for infrastructure projects requiring compliance with MIL-SPEC or Eurocode standards for extreme thermal or seismic environments, the intrinsic stability of thermal fusion remains the gold standard. Project managers must determine if the "speed-to-market" offered by UV curing outweighs the "century-long durability" potential of thermal methods, particularly when integrating nano-layered EMI shielding gaskets or carbon-fiber-reinforced polymers (CFRP).
Critical Application Scenarios: Aerospace vs. Civil Infrastructure
In the aerospace sector, where weight reduction and electromagnetic interference (EMI) shielding are paramount, UV curable adhesives are frequently used for tacking and sealing shielding gaskets. These materials must maintain their conductivity and flexibility throughout the aircraft's lifecycle. The ability of UV adhesives to cure "on demand" allows operators to perfectly position complex gaskets before initiating the 10-second curing cycle. This level of precision is essential when working with nano-layered materials that are susceptible to damage from the sustained heat cycles associated with traditional thermal bonding.
Conversely, in heavy civil infrastructure, such as the installation of lead-rubber seismic bearings or large-scale expansion joints, thermal bonding is often the only viable solution. These components must withstand massive compressive loads and lateral displacements during seismic events. The bond interface must be as strong as the Grade 12.9 specialized bolts that secure them. Thermal fusion provides a deep molecular bond that can resist the ingress of moisture and corrosive agents, ensuring the integrity of the structure for over 75 years without requiring frequent structural repair intervention.
A third scenario involves the repair of composite materials like CFRP (Carbon-Fiber-Reinforced Polymers) in bridge decks or stadium roofs. Here, G-SCE engineers often recommend a hybrid approach. UV adhesives may be used for initial positioning and temporary fixation, followed by a targeted thermal post-cure to maximize the cross-linking density. This 2-stage approach ensures both the speed required for minimizing traffic disruption and the ultimate strength required for public safety. For technical evaluators, understanding how to combine these techniques can lead to a 15-25% reduction in overall project maintenance costs over the asset's lifespan.
EMI Mitigation and Shielding Considerations
For projects involving electronic assets and telecommunications towers, EMI mitigation is a non-negotiable requirement. UV curable adhesives can be formulated with conductive fillers like silver or nickel, but the curing process must not interfere with the particle-to-particle contact necessary for conductivity. Thermal bonding, through its higher pressure and temperature, often creates a more consolidated conductive path. Decision-makers must evaluate the shielding effectiveness—typically required to be >60 dB across a broad frequency spectrum—when selecting their assembly method to ensure full regulatory compliance with international electronic protection standards.
Compliance, Standards, and Regulatory Benchmarking
Navigating the complex landscape of international standards is a core responsibility for project managers and safety officers. Adhesives used in structural connectors must often meet ASTM D903 for peel strength and ASTM D1002 for lap shear strength. For UV curable materials, the stability of the photoinitiator system under long-term UV exposure (solar radiation) is a critical concern. At G-SCE, we benchmark these materials through accelerated weathering tests, simulating 20 years of UV exposure in 1,000 hours of intensive lab testing to ensure that the "Structural Durability" is not just a marketing claim but a verified technical reality.
Thermal bonding processes are governed by a different set of certifications, particularly in the European market where Eurocode 3 and 4 dictate the requirements for steel-to-concrete and composite connections. These standards focus heavily on the fatigue life of the joint and its performance under fire-rated conditions. Because thermal bonding often involves high-energy processes, certifications such as ISO 3834 (Quality requirements for fusion welding) may be applicable, even for non-metallic bonding, to ensure that the process parameters—temperature, pressure, and time—are consistently met across 100% of the production run.
The following benchmarking table highlights the key regulatory frameworks that decision-makers must consider when evaluating these technologies for global infrastructure assets.
For procurement directors, selecting a vendor that provides full documentation for these standards is essential for risk mitigation. A typical certification package for structural adhesives should include the batch-specific Certificate of Analysis (COA) and a detailed Material Safety Data Sheet (MSDS). Failure to verify these documents can lead to significant delays during the 3-stage site inspection and handover phase, potentially resulting in millions of dollars in liquidated damages for large-scale engineering conglomerates.
Frequently Asked Questions (FAQ)
Can UV curable glue replace thermal bonding in all applications?
No, UV curable glue cannot replace thermal bonding in every scenario, particularly where the substrates are opaque or where deep-section curing is required beyond 5mm to 10mm. While UV methods offer superior speed, thermal bonding remains the standard for creating high-homogeneity bonds in thick structural members or where the service environment exceeds 180°C. For decision-makers, the choice should be based on the specific thermal and geometric constraints of the assembly rather than just the desire for faster throughput.
How do environmental conditions affect the curing process?
Environmental factors such as ambient humidity and temperature can significantly impact both methods. High humidity (>65%) can inhibit the curing of some UV resins, while extreme cold can lead to thermal shock during the cooling phase of thermal bonding. It is recommended to maintain a controlled cleanroom or semi-controlled fabrication environment with a temperature of 20°C to 25°C to ensure consistent bond strength and to avoid the formation of micro-voids in the adhesive layer.
What are the typical lead times for specialized assembly equipment?
For standard UV LED curing stations, the typical lead time is 2 to 4 weeks. However, for large-scale industrial thermal bonding systems or custom-designed induction heating arrays, procurement managers should budget for a lead time of 12 to 24 weeks. This timeline must include the 2-week period required for site installation, calibration, and personnel training to ensure compliance with occupational safety and shielding protocols on the manufacturing floor.
Strategic Procurement and Technical Advisory with G-SCE
In the high-stakes world of global infrastructure, the difference between a successful project and a multi-billion dollar liability often comes down to the choice of a single bonding material or fastening system. The Global Structural-Connectors & Extreme-Shielding (G-SCE) hub provides the technical depth and regulatory oversight required to make these decisions with absolute confidence. Our multidisciplinary team of structural engineers and material scientists is dedicated to benchmarking the world's most critical assets against the highest international standards, ensuring that every Grade 12.9 bolt and every nano-layered shielding gasket performs as designed for its entire lifecycle.
Whether you are a Chief Infrastructure Officer overseeing a 50-year mega-structure project or a Procurement Director sourcing high-performance adhesives for aerospace applications, G-SCE offers an uncompromising perspective on the integrity of infrastructure. We invite you to leverage our repository of technical data and benchmarking reports to optimize your material fabrication and shielding protocols. Our services are designed to bridge the gap between material science and engineering reality, providing the safety and reliability that modern engineering projects demand.
Contact our technical advisory team today to discuss your specific requirements. We provide expert consultation on the following critical areas:
- Custom Benchmarking of UV Curable vs. Thermal Bonding for specific substrate combinations.
- Validation of compliance for ISO, ASTM, and MIL-SPEC certifications.
- Development of 3-stage quality control protocols for site-wide structural repair and assembly.
- Consultation on EMI shielding effectiveness for high-stakes electronic assets.
- Technical auditing of procurement pipelines for Grade 12.9 fasteners and seismic isolation units.
- Structural Connectors
- Seismic Isolation
- EMI Shielding
- Structural Reinforcement
- Nano-Layered Shielding
- High-Performance Adhesives
- Seismic Bearings
- Material Fabrication
- Structural Repair
- Shielding Protocols
- Engineering Materials
- Structural Safety
- Industrial Fasteners
- Seismic Protection
- EMI Mitigation
- Infrastructure Materials
- Structural Durability
Recommended News
Quarterly Executive Summaries Delivered Directly.
Join 50,000+ industry leaders who receive our proprietary market analysis and policy outlooks before they hit the public library.